
Quality & Inspection
Checked against
your drawing.
Dimensional, appearance and functional checks planned around your part and agreed acceptance criteria.
CMM inspection Dimensional & geometric verification
Our Certifications
Certificates and inspection reports, available for your review.


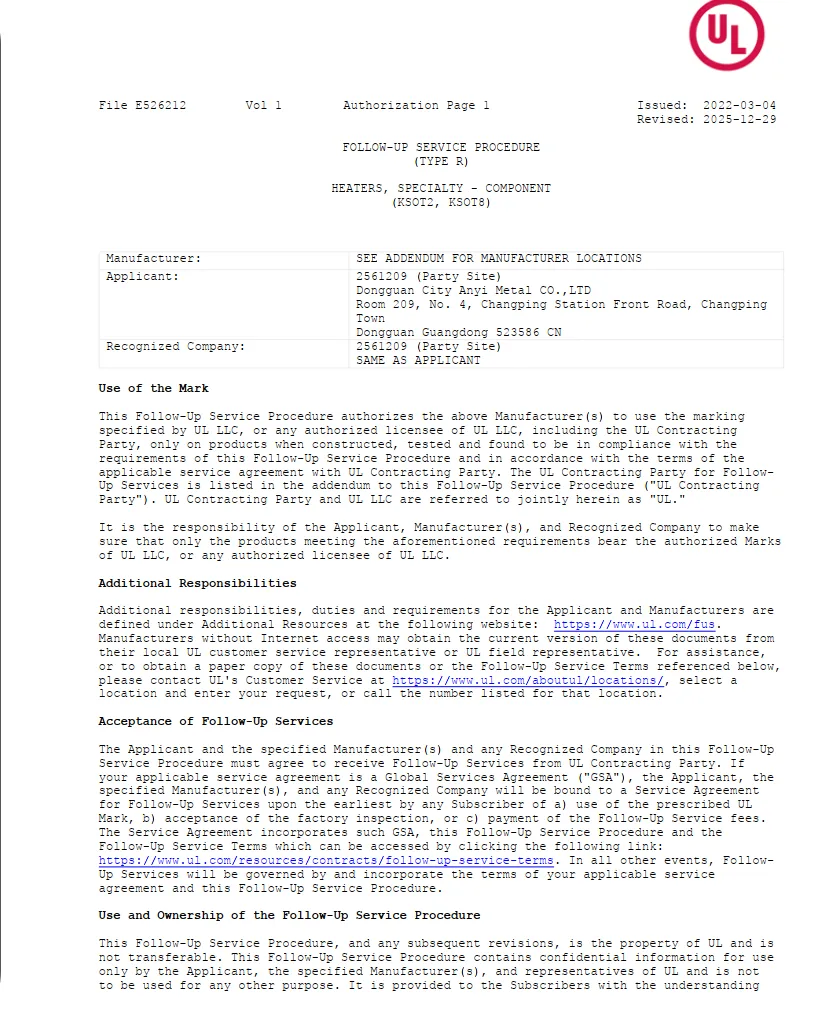
Swipe to view more
Dimensional & functional inspection
4 CMM systems 3 vision measuring systems
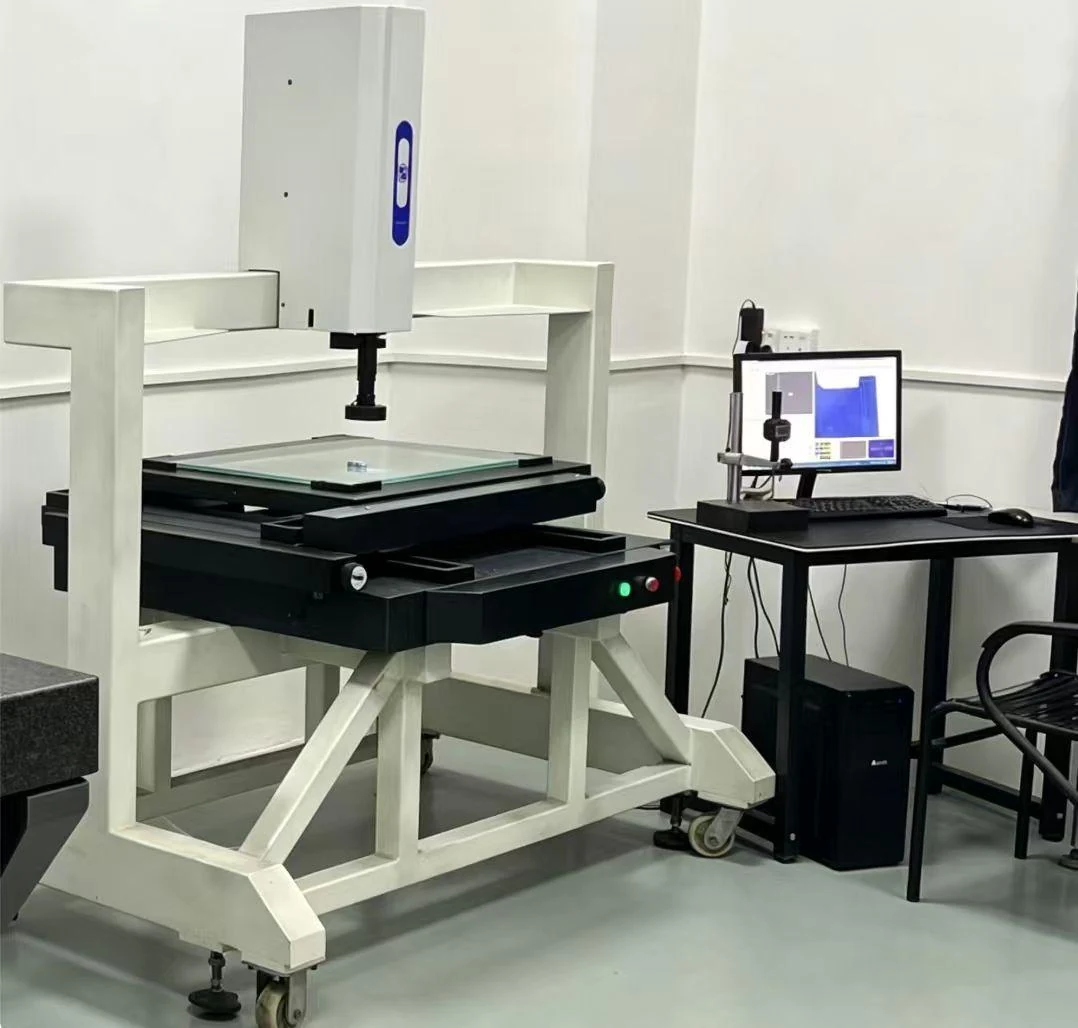
Vision Measuring
Optical dimensions and profiles.
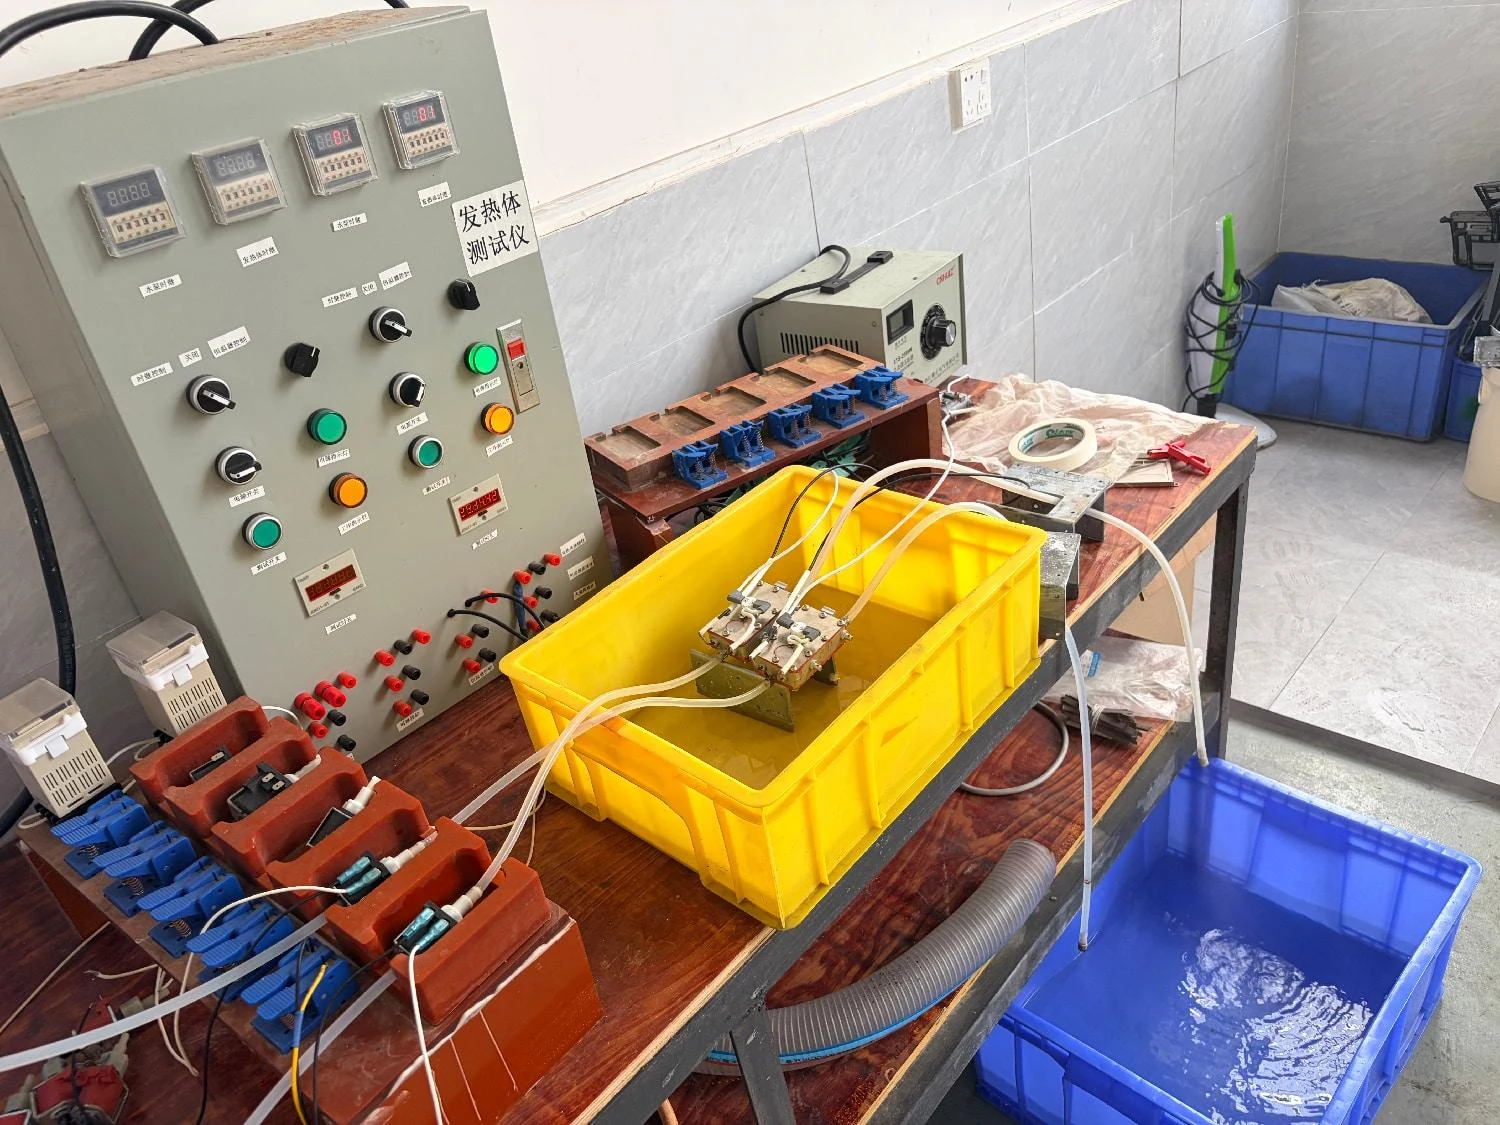
Electrical Testing
Specified checks for heating components.
Appearance inspection by surface zone
We agree surface zones, appearance references and defect limits for your part before production.
- Surface marks
- Assess scratches, dents and visible spots against the approved appearance and limit samples.
- Edges & form
- Check burrs, gate trimming and deformation. Verify flatness where specified.
- Colour & coating
- Compare colour with the approved reference and inspect for bubbles, pinholes or peeling.
- Logos & markings
- Check clarity, position and alignment against the drawing and approved reference.
Approved reference samples
Inspectors compare parts with the agreed appearance reference and limit samples. Inspection decisions follow the criteria for each surface zone.
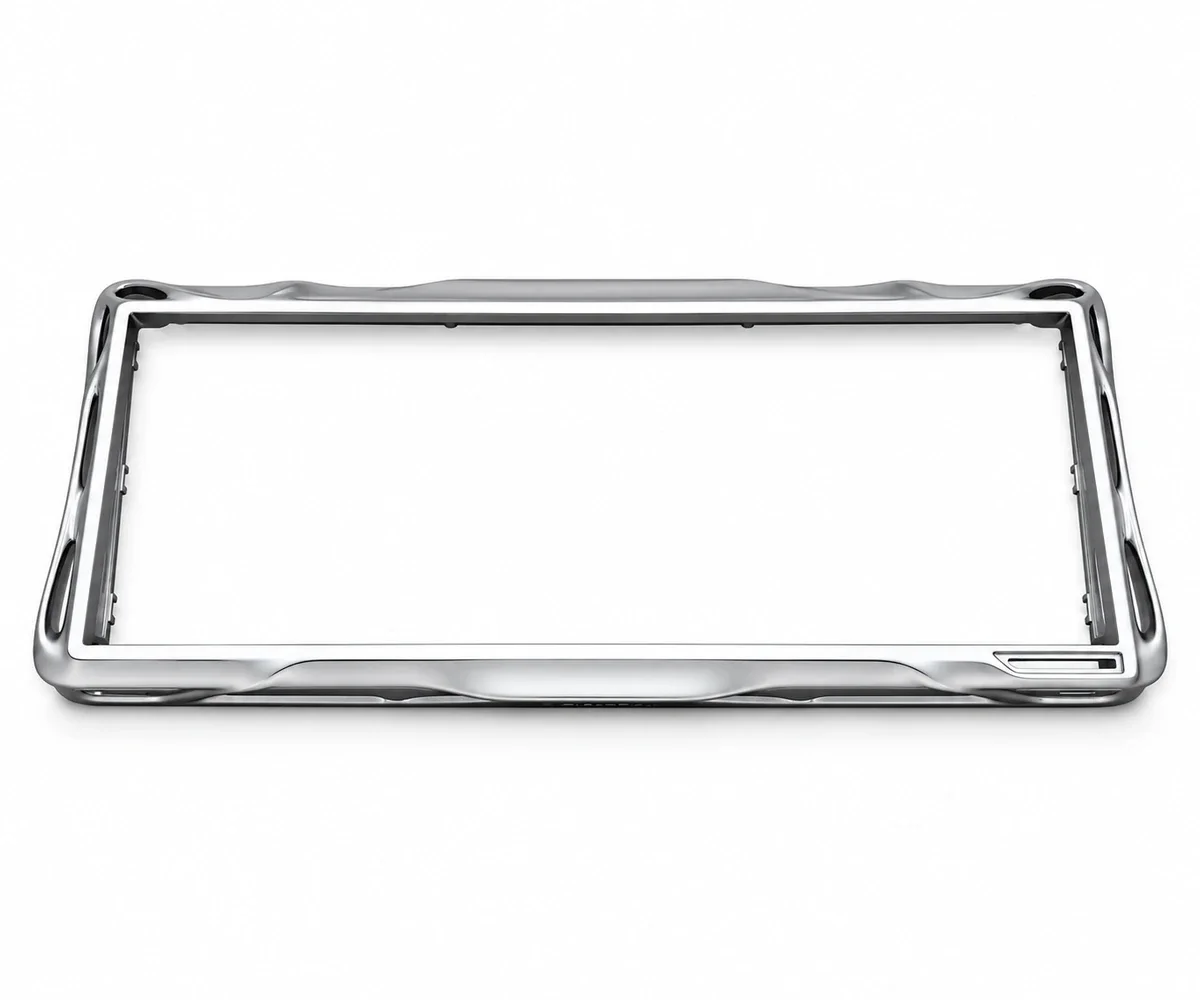
Part-specific surface zones
- A
- B
- C
- D
Zone definitions and acceptance limits are confirmed for each part.
Surface finish verification
Paint and powder coating have different requirements. We define the finish reference, test method and acceptance limits for the specified process.
- Coating thickness
- Measure the coating against the specified thickness range.
- Colour consistency
- Compare with the approved colour reference, with instrumental checks where specified.
- Adhesion
- Use the specified cross-cut and tape test to assess coating adhesion.
- Corrosion resistance
- Carry out salt spray testing for the agreed duration and assessment criteria.

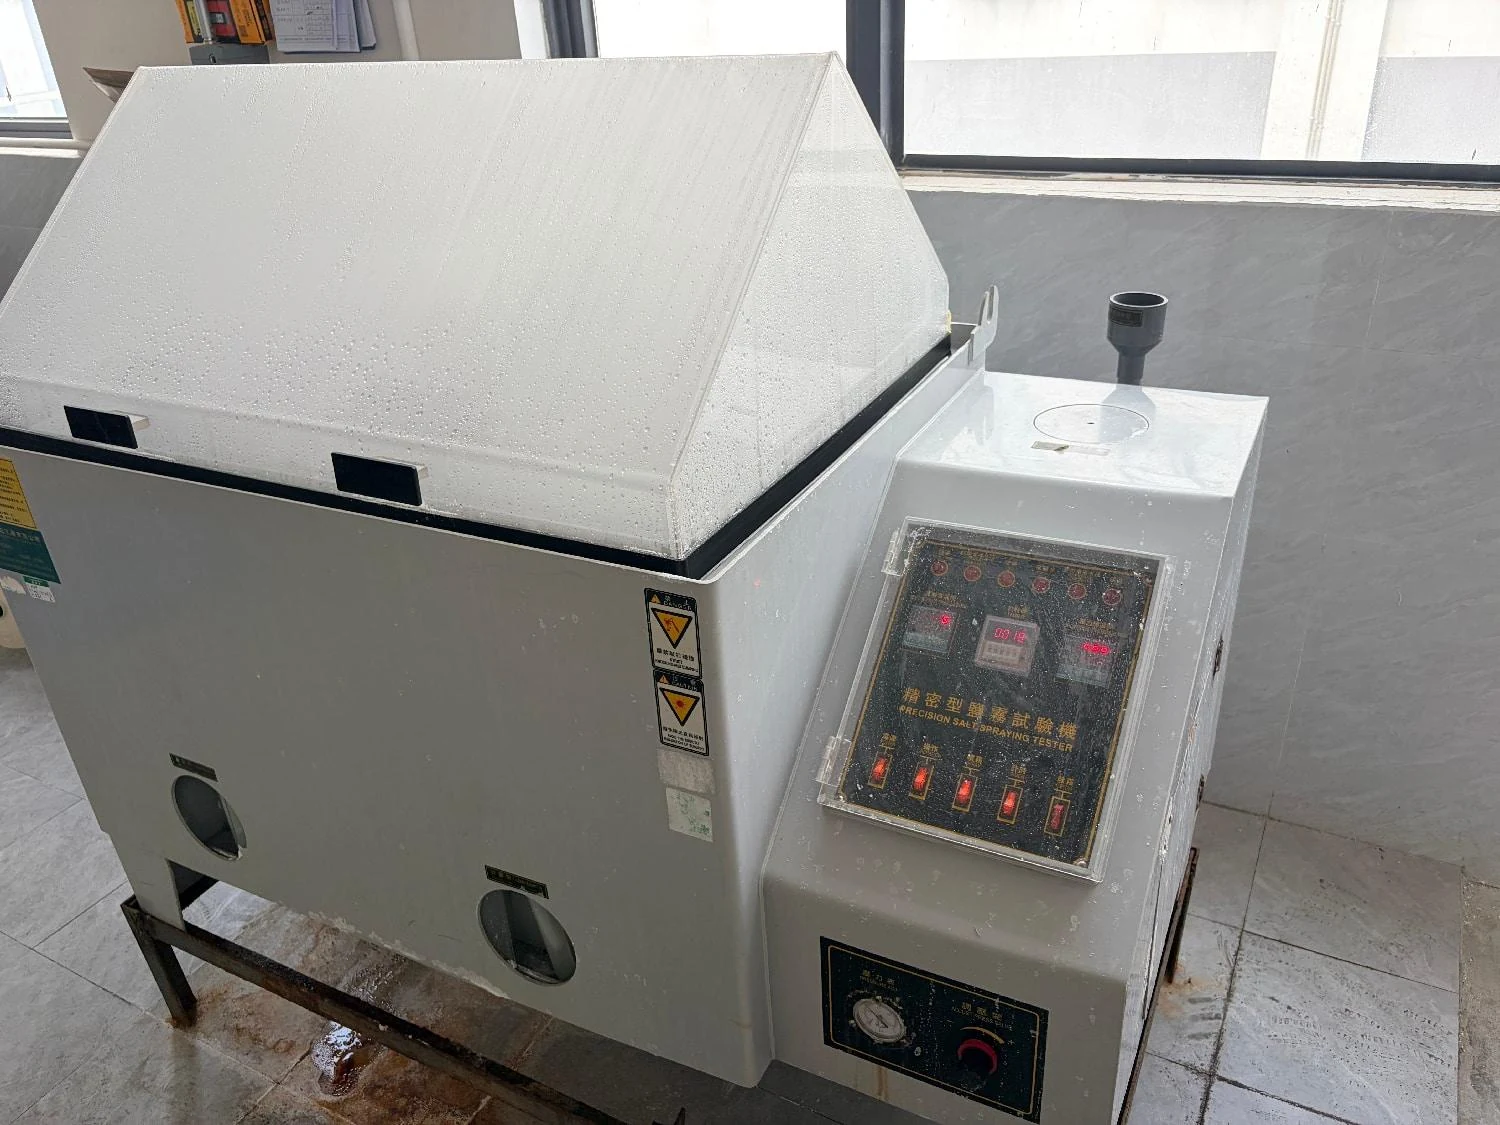
Test frequency, specimen selection and pass criteria are confirmed for the coating and part. Additional checks, such as pencil hardness or alcohol resistance, can be specified.
See surface finishing capabilitiesLeak testing for sealed housings
For parts with sealing requirements, dedicated fixtures and part-specific test settings help check for leaks during production.
Daily reference checks
Check the test equipment with known acceptable and rejected reference parts before continuing production.
Part-specific test conditions
Define the fixture, test pressure, hold time and acceptance limit for the part and its sealing requirements.
Individual checks & segregation
Parts on the specified leak-test route are checked individually. Rejected parts are identified and kept separate.
Leak inspection sequence
- Verify the setupConfirm the fixture and reference checks.
- Position & seal the partSeat the part correctly without damaging its surfaces.
- Pressurise & holdApply the conditions specified for the part.
- Evaluate & separateRelease acceptable parts and segregate rejects.
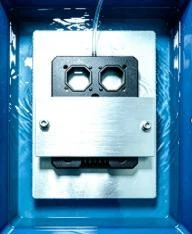
First-piece, in-process and last-piece checks follow the specified inspection plan. Test coverage and required records are agreed for your project.
See assembly and testing capabilitiesProduct protection through handling and packing
The packing method follows the part geometry, finished surfaces and agreed shipping requirements.
Inspect before packing
Only accepted parts move into final packing. Check appearance, finish and the specified dimensions against the agreed reference.
Separate individual parts
Use the specified formed trays, protective bags or wrapping to prevent contact between vulnerable surfaces.
Protect each layer
Use the defined separators and handling method during transfer. Keep rejected parts identified and stored separately.
Check quantity and labels
Confirm the packing quantity and match the label to the contents before closing the container.
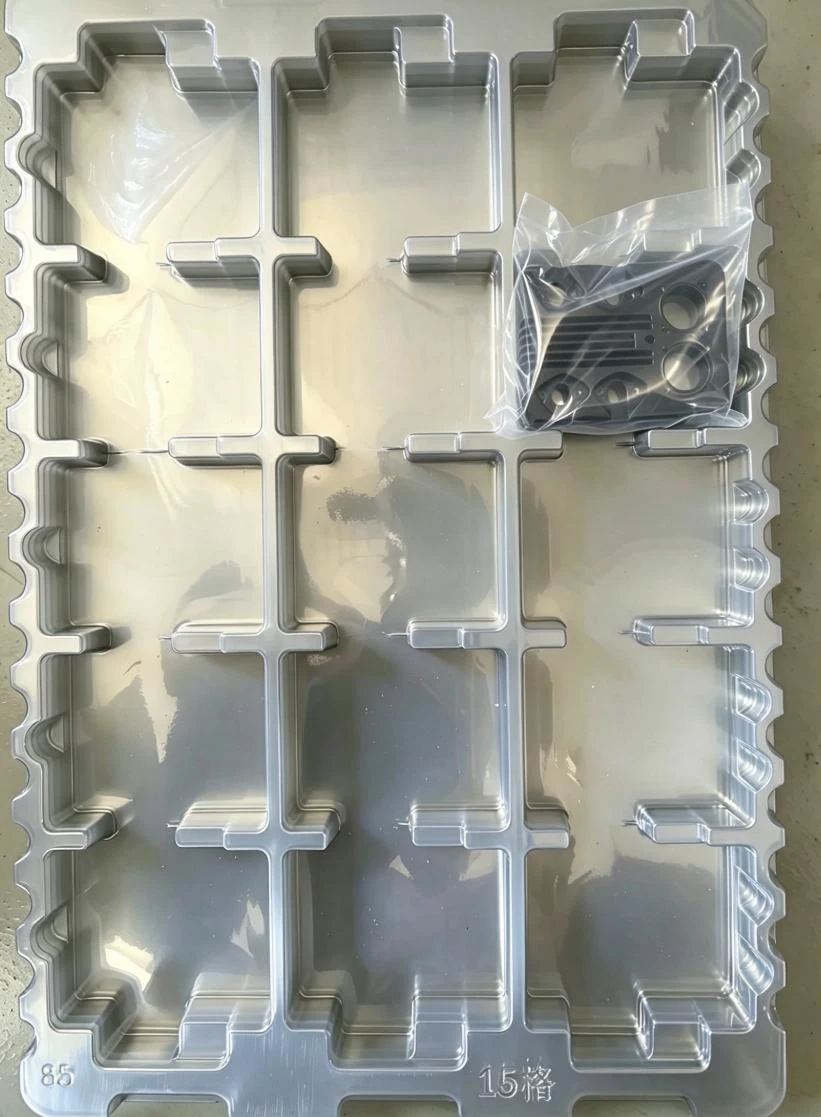
Part-specific packing: tray design, protective materials and quantities are confirmed for each project.